Omron 61F-G2NH Elevates High-Purity Liquid Level Control for Industrial Applications
Industrial Automation News
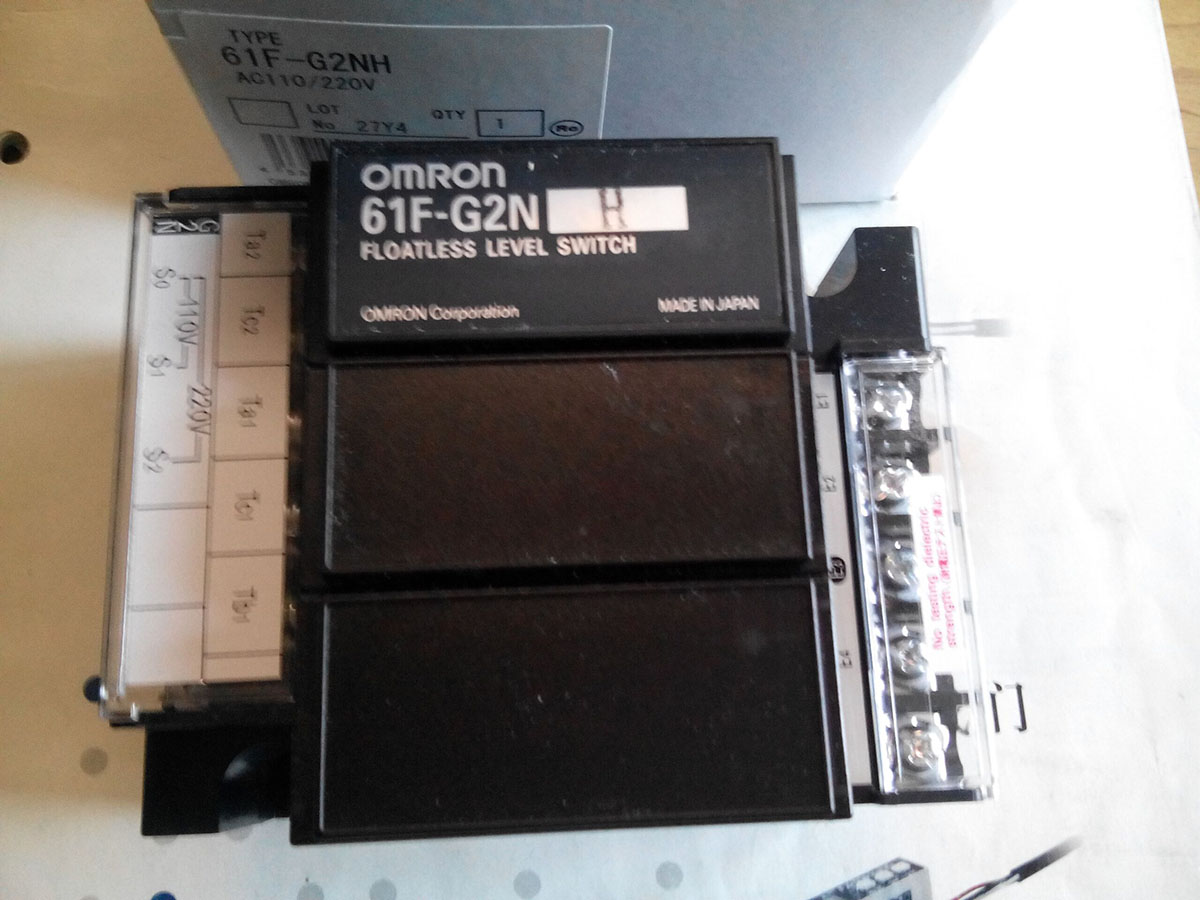
Omron has upgraded its industrial level control lineup with the launch of the 61F-G2NH floatless level switch, a high-sensitivity solution tailored for precise and stable liquid level detection of high-resistivity pure water. Optimized for water treatment, pharmaceutical processing, food and beverage production, and precision manufacturing environments, the new device addresses the long-standing detection inaccuracies of conventional level controllers in high-purity liquid scenarios.
Different from traditional mechanical float switches, the 61F-G2NH adopts electrode-type non-float detection technology, completely eliminating mechanical wear, float jamming and frequent maintenance issues caused by movable components. With a professional working resistance range of 10kΩ to 40kΩ, the device achieves reliable level monitoring for distilled water, deionized water and other high-resistivity media that ordinary level switches fail to identify stably, filling the demand gap for high-precision liquid level control in pure water industrial systems.
Integrating dual core functions of automatic operation and safety warning, the 61F-G2NH supports intelligent automatic water supply and drainage pump control, realizing unattended automatic operation of liquid storage tanks. Meanwhile, it is equipped with a high-level overflow alarm function. When the liquid level exceeds the preset safety threshold, the device will immediately output a relay alarm signal to effectively prevent tank overflow, liquid leakage and equipment safety risks, greatly improving the safety and stability of industrial fluid control systems.
Designed for industrial standard installation, the model supports both panel mounting and DIN rail mounting, featuring flexible and convenient on-site deployment. It adapts to a universal AC 100/200V wide voltage power supply with 85% to 110% rated voltage fluctuation tolerance, ensuring stable operation in complex industrial power environments. The equipment features low power consumption below 4VA, achieving energy-saving operation while maintaining efficient performance. Its output contact can bear 200V AC and 3A resistive load, meeting the driving demand of most industrial pump equipment and alarm devices.
In terms of environmental adaptability and on-site operation, the 61F-G2NH works stably in an ambient temperature range from -10°C to +55°C, suitable for most indoor industrial control cabinet working conditions. The built-in LED status indicator clearly displays the equipment operating state, facilitating real-time status observation and rapid fault diagnosis for on-site technicians. The modular integrated structure simplifies daily replacement and maintenance procedures, reducing equipment downtime and later operation costs for enterprises.
Industry analysts pointed out that the 61F-G2NH perfectly balances high detection accuracy, operational stability and low maintenance cost. As a professional dedicated controller for high-purity liquid level control, it will further optimize the automated fluid control process in fine manufacturing and biopharmaceutical industries, providing more reliable basic equipment support for industrial production upgrading and intelligent transformation.